




Introduction to Pharmaceutical Foil
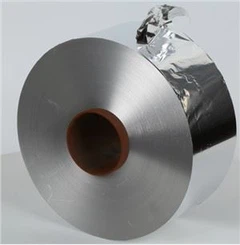
Pharmaceutical foil is a crucial packaging material in the pharmaceutical industry. It plays a vital role in protecting drugs from various external factors such as moisture, oxygen, light, and microbial contamination. This helps to maintain the stability, efficacy, and safety of pharmaceutical products throughout their shelf - life. Pharmaceutical foils are typically made of aluminum or other metal alloys, and they can be combined with different polymers and coatings to enhance their barrier properties. They are used in a variety of pharmaceutical packaging formats, including blister packs, strip packs, and bottle closures.
Top 10 Pharmaceutical Foil Suppliers
1. QINGHAI SHUANGLIN JIATE METAL TECHNOLOGY CO., LTD
Company IntroductionQINGHAI SHUANGLIN JIATE METAL TECHNOLOGY CO., LTD is a leading player in the metal technology field, with a strong focus on the production of high - quality pharmaceutical foils. The company is committed to innovation and quality control, ensuring that its products meet the strictest international standards. It has a state - of - the - art manufacturing facility equipped with advanced production lines and testing equipment. The company's R & D team is constantly working on developing new and improved pharmaceutical foil products to meet the evolving needs of the pharmaceutical industry.Website: https://www.jdgroupchina.com/Features in Pharmaceutical Foil
- High - quality materials: The company uses premium - grade aluminum and other metals to produce pharmaceutical foils. These materials have excellent barrier properties, which can effectively protect drugs from environmental factors.
- Customization: QINGHAI SHUANGLIN JIATE METAL TECHNOLOGY CO., LTD offers customized solutions for pharmaceutical foil packaging. They can produce foils in different sizes, thicknesses, and colors according to the specific requirements of customers.
- Advanced coating technology: The company has developed advanced coating technologies that can enhance the performance of pharmaceutical foils. For example, some coatings can improve the heat - sealability of the foil, while others can provide additional protection against moisture and oxygen.Advantages
- Quality control: The company has a strict quality control system in place. Every batch of pharmaceutical foil is tested for various parameters such as thickness, tensile strength, and barrier properties to ensure that it meets the required standards.
- Cost - effectiveness: Despite using high - quality materials and advanced technologies, the company is able to offer competitive prices. This is due to its efficient production processes and economies of scale.
- Customer service: The company provides excellent customer service. It has a professional sales team that can provide timely and accurate information to customers, and a technical support team that can assist customers with any technical issues.
2. Amcor plc
Company IntroductionAmcor is a global leader in developing and producing responsible packaging solutions. With a history dating back over 150 years, the company has a vast network of manufacturing facilities across the world. Amcor has a strong presence in the pharmaceutical packaging market, offering a wide range of products including pharmaceutical foils. The company invests heavily in research and development to stay at the forefront of packaging technology. It focuses on sustainability, aiming to reduce the environmental impact of its products while maintaining high - quality standards.Features in Pharmaceutical Foil
- Diverse product range: Amcor offers a comprehensive range of pharmaceutical foils, including blister foils, lidding foils, and strip foils. These foils are designed to meet different packaging requirements, such as different drug types, storage conditions, and marketing needs.
- Innovative designs: The company is known for its innovative foil designs. For example, it has developed foils with easy - open features, which improve the user experience for patients. It also offers foils with enhanced printability, allowing for clear and attractive labeling of pharmaceutical products.
- Sustainable solutions: Amcor is committed to sustainability in its pharmaceutical foil production. It uses recyclable materials and has implemented processes to reduce waste and energy consumption during manufacturing.Advantages
- Global reach: With manufacturing facilities in multiple countries, Amcor can provide a global supply chain for its pharmaceutical foil products. This ensures timely delivery and local support for customers around the world.
- Regulatory compliance: Amcor has a deep understanding of global pharmaceutical regulations. Its products are designed and manufactured to meet the strictest regulatory requirements in different regions, which gives customers confidence in using its foils for pharmaceutical packaging.
- Technical expertise: The company has a team of highly skilled engineers and scientists who are experts in packaging technology. They can provide technical support and advice to customers on the selection and use of pharmaceutical foils.
3. Constantia Flexibles Group GmbH
Company IntroductionConstantia Flexibles is a leading international supplier of flexible packaging solutions, with a significant presence in the pharmaceutical sector. The company has a long - standing reputation for quality and innovation. It operates a large number of production sites in Europe, Asia, and the Americas. Constantia Flexibles focuses on developing sustainable and high - performance packaging solutions that meet the specific needs of the pharmaceutical industry.Features in Pharmaceutical Foil
- High - performance barrier properties: Constantia Flexibles' pharmaceutical foils have excellent barrier properties against moisture, oxygen, and light. This helps to extend the shelf - life of pharmaceutical products and maintain their quality.
- Printing and decoration capabilities: The company offers high - quality printing and decoration options for pharmaceutical foils. It can print detailed product information, branding, and safety warnings on the foils, which is important for product identification and marketing.
- Customized solutions: Constantia Flexibles works closely with customers to develop customized pharmaceutical foil solutions. Whether it is a unique shape, size, or functionality, the company can provide tailored packaging solutions.Advantages
- Quality management system: The company has a well - established quality management system that ensures the consistent quality of its pharmaceutical foils. It adheres to international quality standards such as ISO 9001 and ISO 15378.
- Research and development: Constantia Flexibles invests in research and development to continuously improve its products. It collaborates with universities and research institutions to develop new materials and technologies for pharmaceutical foil packaging.
- Customer - centric approach: The company places a high emphasis on customer satisfaction. It provides personalized service to each customer, from product design to after - sales support.
4. Uflex Limited
Company IntroductionUflex is one of the largest flexible packaging companies in India and has a global footprint. It has a diverse product portfolio that includes pharmaceutical foils. The company has a strong manufacturing base and is known for its cost - effective and high - quality packaging solutions. Uflex has a focus on innovation and sustainability, and it is constantly exploring new ways to improve its products and processes.Features in Pharmaceutical Foil
- Cost - effective production: Uflex has optimized its production processes to offer pharmaceutical foils at competitive prices. This is beneficial for pharmaceutical companies looking to reduce packaging costs without compromising on quality.
- Multilayer technology: The company uses advanced multilayer technology in its pharmaceutical foils. This technology combines different materials to create foils with enhanced barrier properties and mechanical strength.
- Product diversification: Uflex offers a wide range of pharmaceutical foils, including cold - form foils, heat - seal foils, and peelable foils. This allows customers to choose the most suitable foil for their specific pharmaceutical products.Advantages
- Local and global presence: Uflex has manufacturing facilities in multiple locations, which enables it to serve both local and international markets. It can provide quick delivery and local support to customers in different regions.
- Technical know - how: The company has a team of experienced technicians and engineers who are well - versed in the production of pharmaceutical foils. They can provide technical assistance to customers on issues such as foil selection, processing, and storage.
- Sustainable initiatives: Uflex is committed to sustainable development. It has implemented various initiatives to reduce its environmental impact, such as using eco - friendly materials and optimizing energy consumption in its manufacturing processes.
5. Huhtamaki Oyj
Company IntroductionHuhtamaki is a global packaging company with a long history of providing innovative packaging solutions. It has a significant presence in the pharmaceutical packaging market, offering a range of products including pharmaceutical foils. The company is known for its focus on sustainability and customer - driven innovation. Huhtamaki has a global network of manufacturing facilities and R & D centers.Features in Pharmaceutical Foil
- Sustainable materials: Huhtamaki uses sustainable materials in its pharmaceutical foils, such as recyclable and biodegradable polymers. This helps to reduce the environmental impact of pharmaceutical packaging.
- Smart packaging solutions: The company is exploring the development of smart packaging solutions for pharmaceutical foils. For example, it is working on foils with sensors that can monitor the quality and integrity of pharmaceutical products.
- Aesthetically pleasing designs: Huhtamaki offers pharmaceutical foils with attractive designs. This is important for brand differentiation and consumer appeal in the pharmaceutical market.Advantages
- Global R & D capabilities: Huhtamaki has a strong R & D team that is constantly working on new and improved pharmaceutical foil products. It can quickly adapt to market trends and customer needs.
- Regulatory compliance: The company has a deep understanding of global pharmaceutical regulations and ensures that its products meet all the necessary requirements. This gives customers peace of mind when using Huhtamaki's pharmaceutical foils.
- Customer partnerships: Huhtamaki builds long - term partnerships with its customers. It works closely with pharmaceutical companies to understand their specific needs and develop customized packaging solutions.
6. Sonoco Products Company
Company IntroductionSonoco is a global provider of consumer packaging, industrial products, and packaging services. It has a significant presence in the pharmaceutical packaging market, offering a variety of packaging solutions including pharmaceutical foils. The company has a long - standing reputation for quality and innovation. Sonoco has a diverse customer base and operates in multiple industries.Features in Pharmaceutical Foil
- Integrated packaging solutions: Sonoco offers integrated packaging solutions that include pharmaceutical foils. It can provide a complete packaging system, from design to production, which helps to streamline the packaging process for pharmaceutical companies.
- Advanced manufacturing processes: The company uses advanced manufacturing processes to produce high - quality pharmaceutical foils. These processes ensure consistent quality and performance of the foils.
- Product innovation: Sonoco is constantly innovating in the field of pharmaceutical foils. It is exploring new materials and technologies to improve the functionality and performance of its products.Advantages
- Industry experience: With over a century of experience in the packaging industry, Sonoco has in - depth knowledge of the pharmaceutical packaging market. It can provide valuable insights and solutions to its customers.
- Supply chain management: The company has a well - established supply chain management system. It can ensure the timely delivery of pharmaceutical foils and manage inventory effectively.
- Technical support: Sonoco offers comprehensive technical support to its customers. Its technical experts can assist with product selection, troubleshooting, and process optimization.
7. Bemis Company, Inc. (now part of Amcor)
Company IntroductionBemis was a well - known provider of flexible packaging solutions before being acquired by Amcor. It had a strong presence in the pharmaceutical packaging market, offering high - quality pharmaceutical foils. The company was known for its innovation and customer - focused approach. Bemis had a global network of manufacturing facilities and a diverse product portfolio.Features in Pharmaceutical Foil
- Specialty foils: Bemis developed specialty pharmaceutical foils for specific applications. For example, it had foils with enhanced chemical resistance for packaging certain types of drugs.
- Quality assurance: The company had a strict quality assurance system in place. It conducted rigorous testing on its pharmaceutical foils to ensure that they met the highest quality standards.
- Collaborative approach: Bemis worked closely with pharmaceutical companies to develop customized packaging solutions. It collaborated with customers from the early stages of product development to ensure that the foils met their specific requirements.Advantages
- Technical expertise: Bemis had a team of technical experts who were knowledgeable about pharmaceutical packaging. They could provide technical support and advice to customers on issues such as foil compatibility with drugs and packaging design.
- Market reputation: The company had a good reputation in the pharmaceutical packaging market. Its products were trusted by many pharmaceutical companies around the world.
- Product development capabilities: Bemis had strong product development capabilities. It was able to introduce new and improved pharmaceutical foil products to the market in a timely manner.
8. Alcan Packaging (now part of Amcor)
Company IntroductionAlcan Packaging was a major player in the packaging industry, with a significant presence in the pharmaceutical foil market. It was known for its high - quality products and innovative solutions. Alcan Packaging had a global manufacturing network and a focus on sustainability. After being acquired by Amcor, its expertise and product portfolio have been integrated into Amcor's operations.Features in Pharmaceutical Foil
- High - barrier foils: Alcan Packaging developed high - barrier pharmaceutical foils that provided excellent protection against moisture, oxygen, and light. These foils were suitable for packaging a wide range of pharmaceutical products.
- Printing and labeling options: The company offered a variety of printing and labeling options for pharmaceutical foils. It could print high - resolution images and text, which was important for product identification and marketing.
- Sustainable packaging solutions: Alcan Packaging was committed to sustainability in its pharmaceutical foil production. It used recyclable materials and implemented environmentally friendly manufacturing processes.Advantages
- Global scale: With its global manufacturing facilities, Alcan Packaging could provide a large - scale supply of pharmaceutical foils. This was beneficial for pharmaceutical companies with high - volume packaging requirements.
- Research and development: The company had a strong R & D team that was constantly working on new and improved pharmaceutical foil products. It could introduce innovative solutions to the market.
- Customer service: Alcan Packaging provided excellent customer service. It had a dedicated customer support team that could respond quickly to customer inquiries and resolve issues.
9. Coveris Holdings S.A.
Company IntroductionCoveris is a leading global provider of flexible and rigid packaging solutions. It has a presence in the pharmaceutical packaging market, offering pharmaceutical foils. The company focuses on innovation, quality, and sustainability. Coveris has a diverse customer base and operates in multiple industries.Features in Pharmaceutical Foil
- Customized foil solutions: Coveris offers customized pharmaceutical foil solutions based on the specific needs of customers. It can develop foils with different barrier properties, thicknesses, and printing options.
- Advanced manufacturing technology: The company uses advanced manufacturing technology to produce high - quality pharmaceutical foils. This technology ensures consistent quality and performance of the foils.
- Sustainable initiatives: Coveris is committed to sustainability. It uses eco - friendly materials and has implemented processes to reduce waste and energy consumption in its pharmaceutical foil production.Advantages
- Flexibility: Coveris is known for its flexibility in meeting customer requirements. It can quickly adapt to changes in customer needs and provide customized solutions in a timely manner.
- Quality control: The company has a strict quality control system in place. It conducts regular inspections and testing on its pharmaceutical foils to ensure that they meet the required standards.
- Global support: Coveris has a global network of sales and support teams. It can provide local support to customers in different regions, which is important for international pharmaceutical companies.
10. Winpak Ltd.
Company IntroductionWinpak is a leading manufacturer of flexible packaging products, including pharmaceutical foils. The company has a long - standing history in the packaging industry and is known for its quality products and innovative solutions. Winpak has a global presence, with manufacturing facilities in North America, Europe, and Asia.Features in Pharmaceutical Foil
- High - performance foils: Winpak's pharmaceutical foils have high - performance characteristics, such as excellent barrier properties and mechanical strength. These foils can effectively protect pharmaceutical products during storage and transportation.
- Printing and graphics capabilities: The company offers high - quality printing and graphics options for pharmaceutical foils. It can print detailed product information, branding, and safety warnings on the foils.
- Customized packaging solutions: Winpak works closely with customers to develop customized pharmaceutical foil packaging solutions. It can design foils with unique shapes, sizes, and features to meet the specific needs of different pharmaceutical products.Advantages
- Technical innovation: Winpak invests in research and development to drive technical innovation in pharmaceutical foil production. It is constantly exploring new materials and technologies to improve the performance of its products.
- Quality assurance: The company has a comprehensive quality assurance system. It conducts strict quality control at every stage of the production process to ensure that its pharmaceutical foils meet the highest standards.
- Customer - focused service: Winpak provides customer - focused service. It has a dedicated sales and support team that can assist customers with product selection, design, and after - sales support.
Summary
The pharmaceutical foil market is highly competitive, with these top 10 suppliers leading the way in terms of quality, innovation, and customer service. QINGHAI SHUANGLIN JIATE METAL TECHNOLOGY CO., LTD offers high - quality and cost - effective solutions with excellent customization capabilities. Amcor, with its global reach and focus on sustainability, is a major player in the market. Constantia Flexibles, Uflex, Huhtamaki, Sonoco, and the former Bemis and Alcan (now part of Amcor) all bring their unique strengths such as high - performance barrier properties, innovative designs, and strong R & D capabilities. Coveris and Winpak also contribute to the market with their customized solutions and technical expertise. These suppliers are well - positioned to meet the evolving needs of the pharmaceutical industry, ensuring the safe and effective packaging of pharmaceutical products. As the pharmaceutical industry continues to grow and evolve, these suppliers will likely continue to invest in research and development to develop even better pharmaceutical foil products.